01 · Development and testing
Before production begins
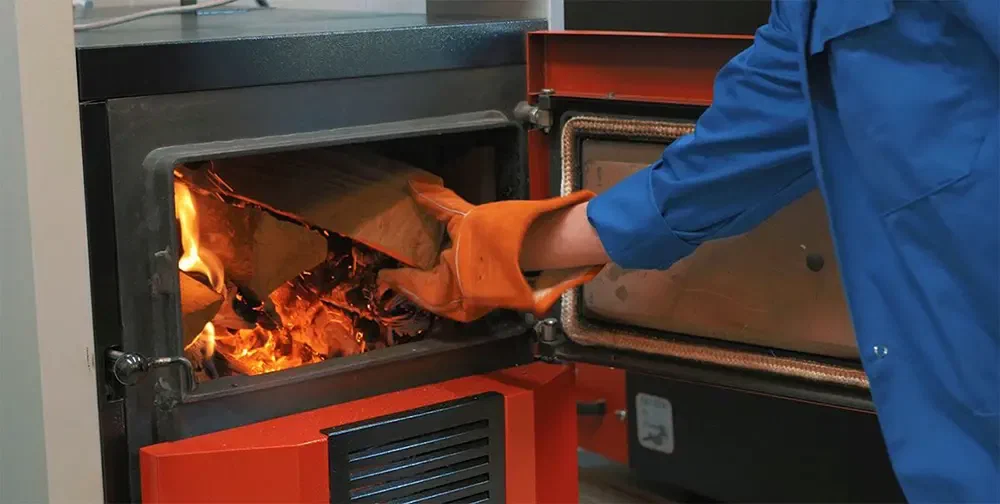
Our in-house development team prepares solutions and checks them through repeated testing. The results help refine the product’s design and function before it enters production.
ATTACK manufacturing · Vrútky
From in-house development to final inspection, we combine specialist expertise, precision technology, and manufacturing in Vrútky.
Explore our manufacturing processManufacturing under one roof
We connect in-house development, digital preparation, steel processing, and final testing in a sequence of coordinated steps. Our certified ISO 9001 system helps maintain quality from the first designs through to dispatch.
In-house energy for manufacturing
The 430 kWp ATTACK photovoltaic power plant supplies energy to manufacturing technologies and product development.
01 · Development and testing
Our in-house development team prepares solutions and checks them through repeated testing. The results help refine the product’s design and function before it enters production.
02 · Digital preparation
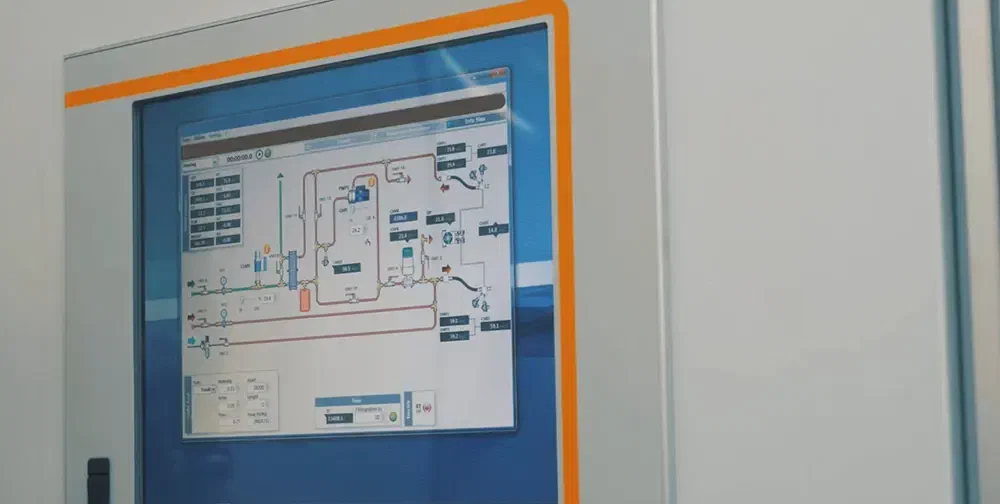
Our specialists define equipment parameters and processing procedures in-house. This keeps our expertise and the continuous improvement of boiler-body manufacturing right here in Vrútky.
03 · Material cutting
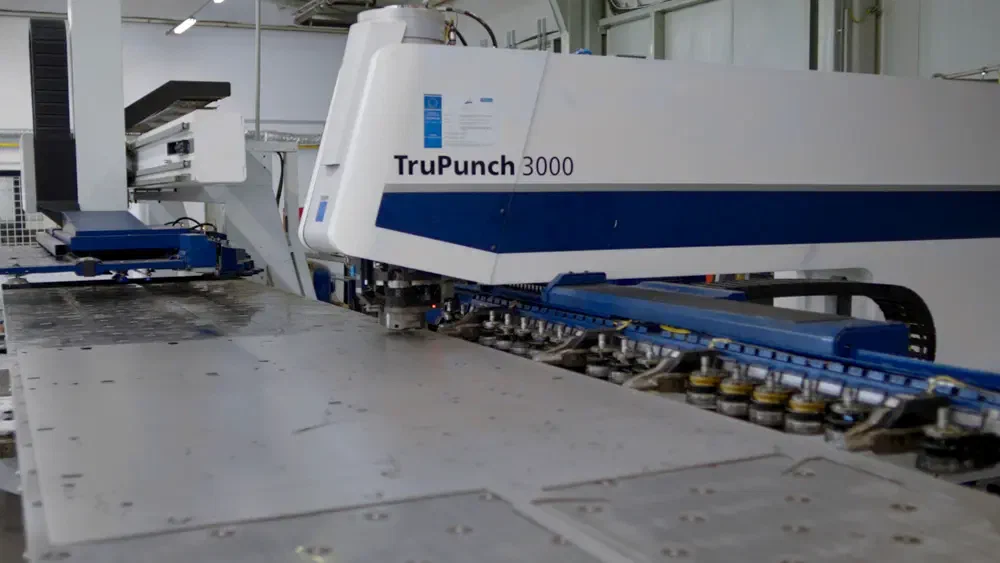
Sheet metal is prepared at automated punching and laser stations. Trumpf, TruLaser, and Bystronic machines process components with high precision; laser output reaches 30 kW, while the Bysprint 3015 delivers up to 20 kW.
04 · Bending
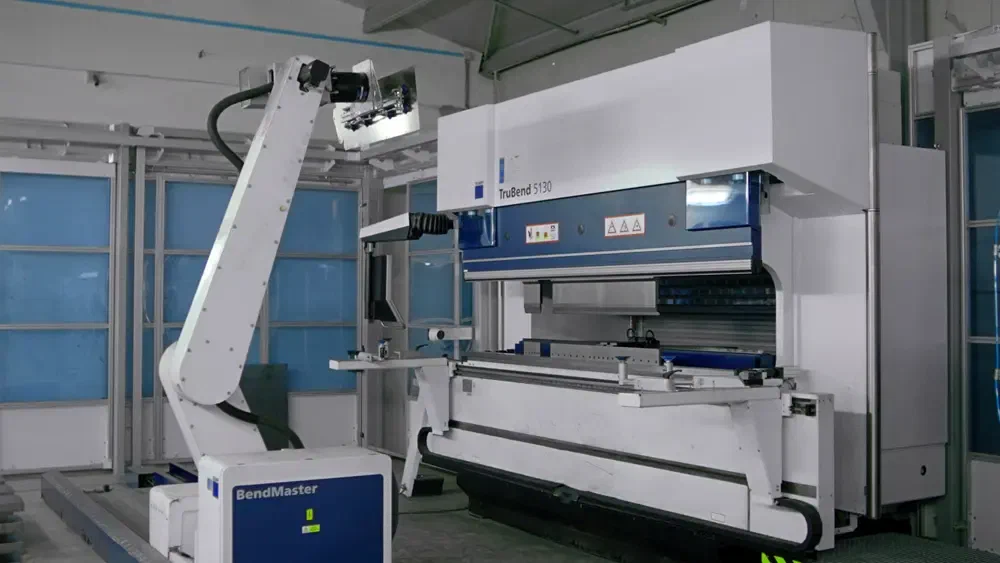
The robotic TruBend 5130 handles large components and operates with a pressing force of up to 130 tonnes. The smaller TruBend 7036 has six backgauge axes for accurate bends in smaller and non-standard parts. Bending is measured by a contact-free laser system. This process delivers high precision and minimal deviation, with efficient, versatile sheet-metal forming.
05 · Welding
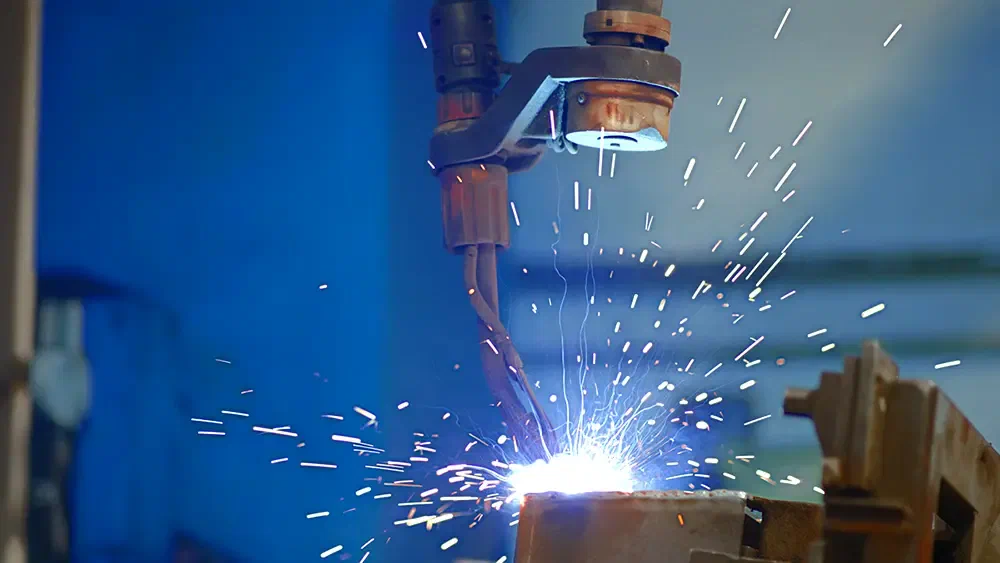
CLOOS robotic CNC stations weld boiler heat exchangers. For other components, we use Kempoweld 4200 and Kempomat 2500 welding systems so each joint meets strength and repeatability requirements.
06 · Pressure testing
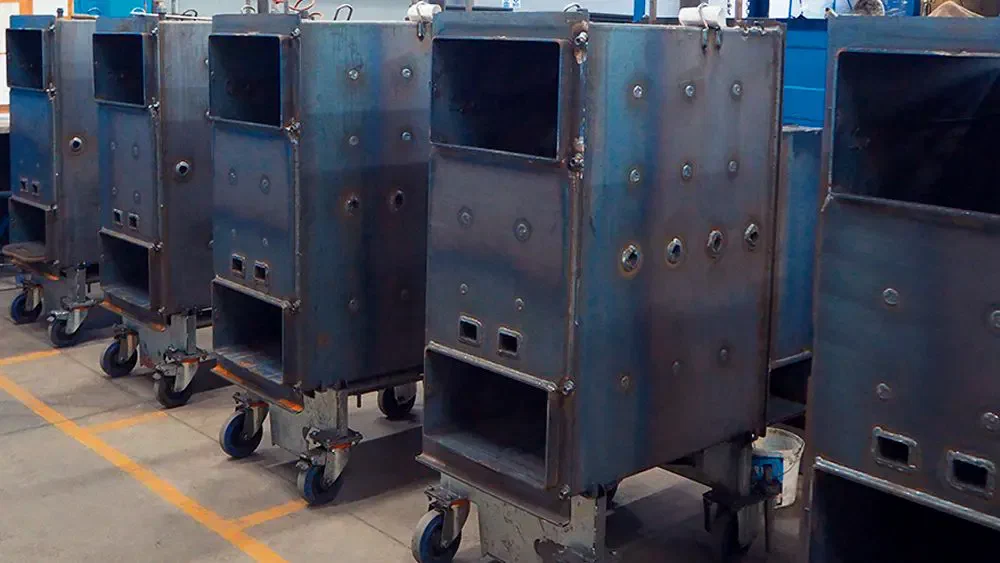
The boiler heat exchanger is tested at 1.5 times the maximum operating pressure. Boiler bodies are checked with air and water at pressures up to 3 MPa; final inspection also includes a functional test of the control system.
07 · Surface treatment
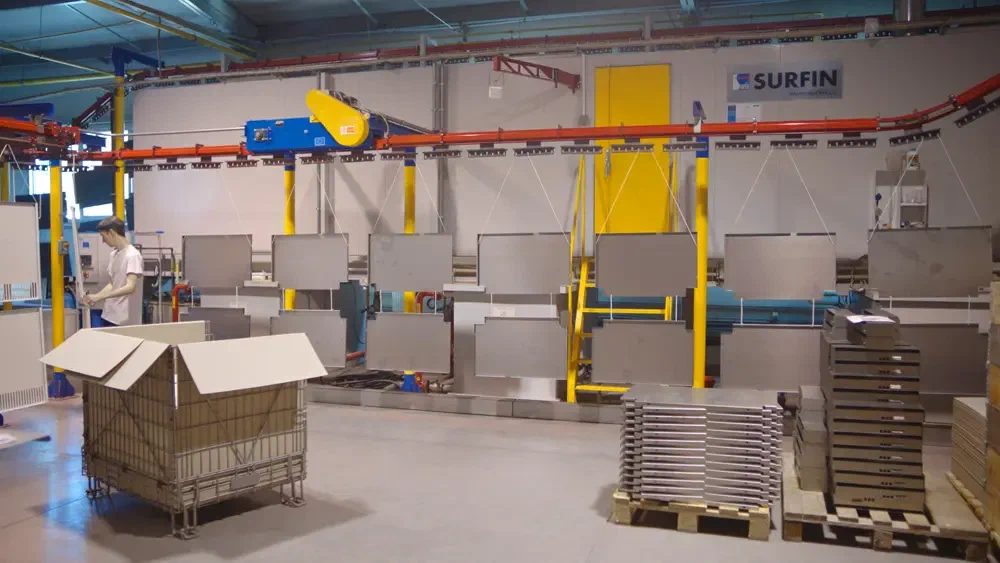
The automated IKP-01 powder-coating line applies an even finish and returns excess powder to the process. Infrared catalytic ovens heat coated parts precisely, reducing unnecessary heat loss.
08 · Assembly and dispatch
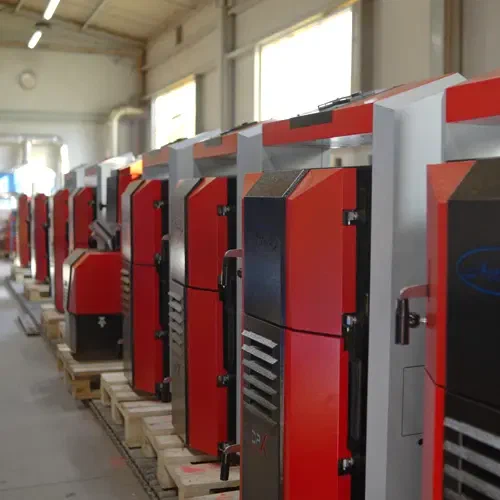
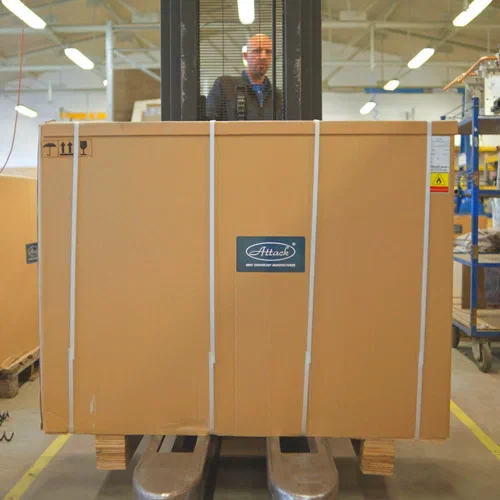
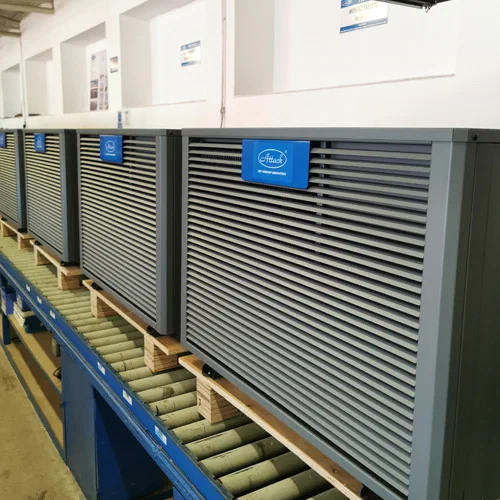
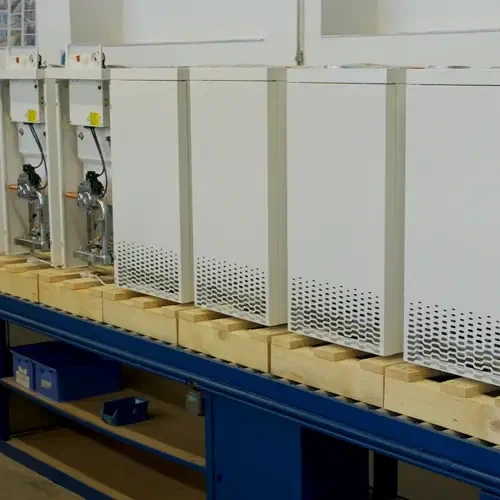
Our assembly lines produce wood, gas, and electric boilers, as well as heat pumps. Each unit is function-tested after assembly and prepared for dispatch to customers.